Answer: A complete bio organic fertilizer production line is configured to cover the entire process—from raw material handling and fermentation/granulation to screening and packaging. The core equipment performs distinct functions and can process various raw materials such as livestock manure, crop straw, and kitchen waste. While equipment configurations remain largely consistent across different production scales, the specifications and output capacities vary; the equipment is categorized into five main groups.
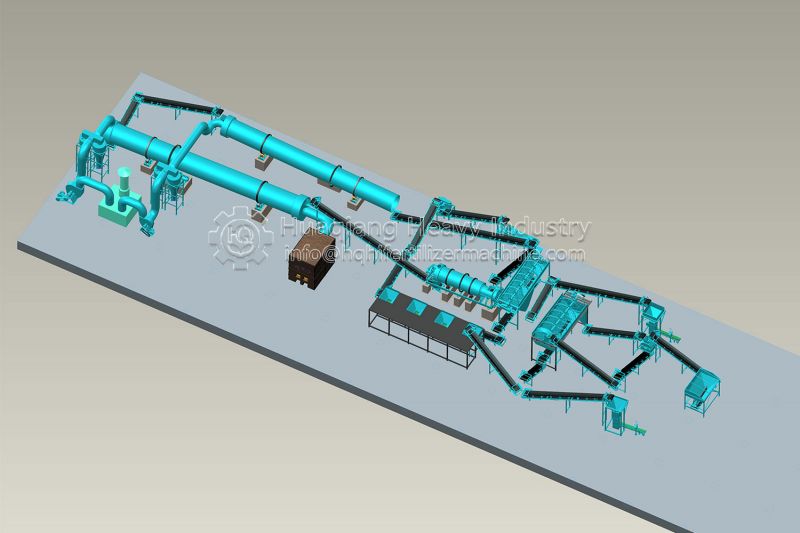
First is the raw material pretreatment equipment, primarily consisting of compost turners, crushers, and screening machines. Compost turners facilitate material turning during fermentation, providing aeration and oxygen, lowering temperatures, and eliminating odors to ensure proper decomposition. Crushers are designed to break down clumps, large raw material chunks, and straw additives, ensuring uniform material fineness and laying the groundwork for subsequent granulation.
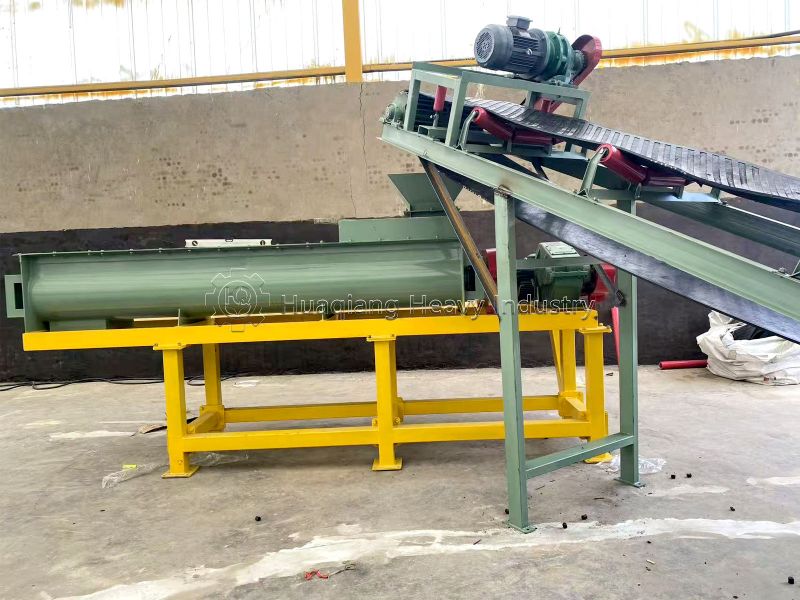
Next is the mixing and proportioning equipment, centered on automatic batching machines and mixers. The automatic batching system precisely proportions decomposed raw materials, microbial inoculants, and trace elements, saving time and labor; the twin-shaft mixer thoroughly blends these materials, ensuring nutrient uniformity and enhancing the quality of the finished fertilizer.
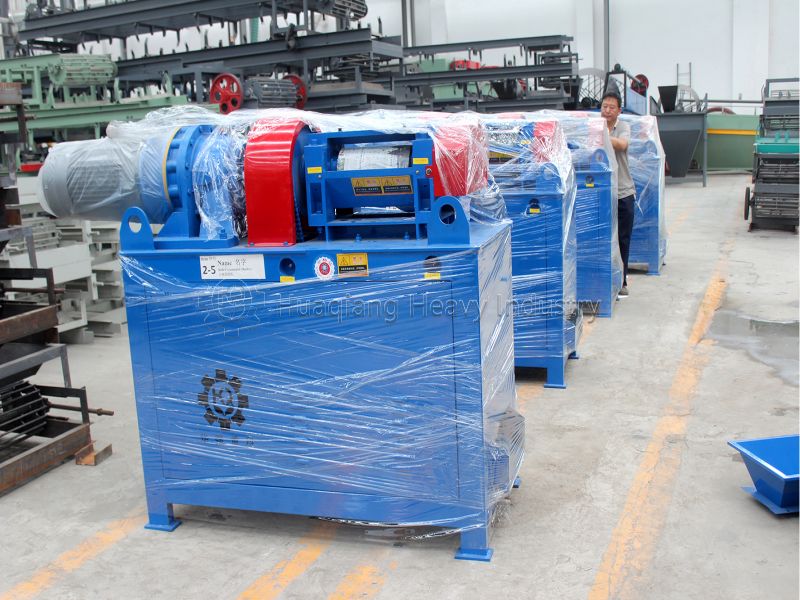
The core forming equipment is the organic fertilizer granulator, a critical component of the production line. Commonly used options include disc granulators and new type organic fertilizer granulators; these transform mixed powdered materials into smooth, uniform granules with high formation rates and optimal hardness, meeting various product specification requirements.
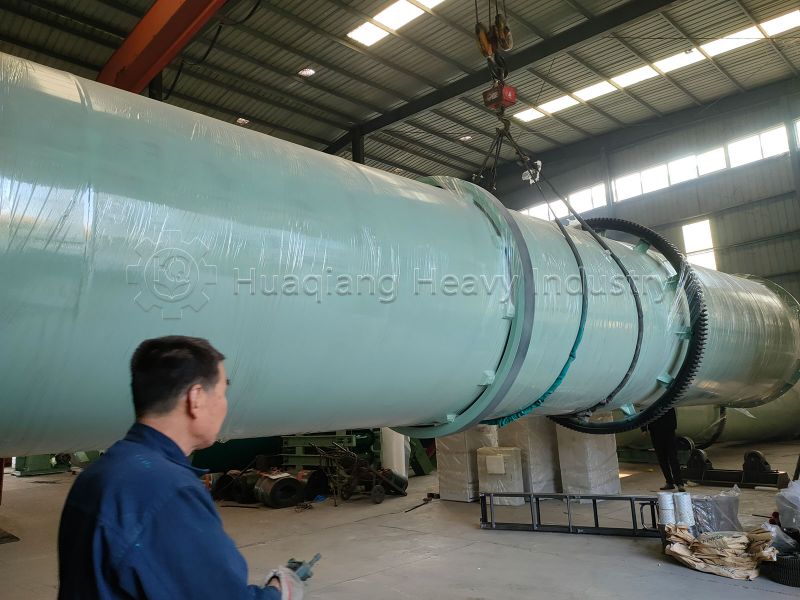
Subsequent equipment includes drying, cooling, and screening units. Dryers reduce granule moisture content to prevent mold and clumping; coolers rapidly lower temperatures to stabilize granule properties; and rotary screening machines separate qualified granules, while undersized fragments and powder are recycled for re-granulation, minimizing raw material waste.
Finally, automatic packaging equipment handles weighing, bagging, and sealing, preparing the finished product for dispatch. This efficient, time-saving system meets the demands of large-scale production. The entire equipment suite can be configured flexibly to suit needs ranging from small-scale facilities to large-scale industrial operations.