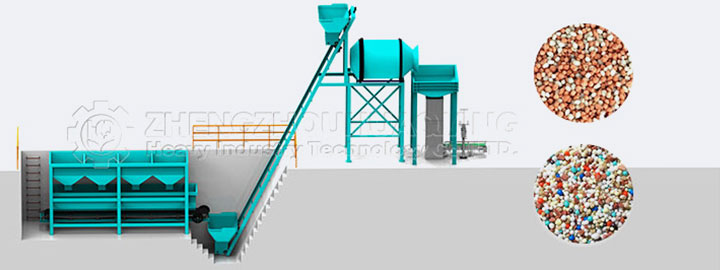
BB fertilizer, also known as blended fertilizer, is produced by physically mixing various granular single-nutrient fertilizers; it requires no granulation or drying processes. The production line centers on precise batching, uniform mixing, and automated packaging. Featuring a streamlined equipment configuration and flexible formula switching, Huaqiang Heavy Industry offers customized solutions tailored to specific production capacity requirements. A complete BB fertilizer production line primarily consists of raw material pre-processing, automated batching, conveying and lifting, mixing, and finished-product packaging.
Raw material pre-processing equipment includes storage silos and vibrating screens. Raw materials—such as urea, potassium chloride, and monoammonium phosphate—are stored in silos equipped with level sensors and anti-bridging devices to prevent the fertilizer from caking or forming "bridges" (clogs). Vibrating screens are used to sift raw materials, break up clumps, and remove impurities, ensuring uniform particle size. This prevents large particles from compromising the accuracy of subsequent batching processes and serves as a foundational step for maintaining consistent product quality.
The automated batching system is the core of the entire production line. It utilizes a multi-bin batching machine integrated with a PLC intelligent control system to weigh and measure various raw materials according to preset formulas. Available in both static and dynamic configurations, the system offers high weighing accuracy and allows for rapid switching between different fertilizer formulas—accommodating the specific fertilization needs of various crops and soil types—while minimizing errors associated with manual batching.
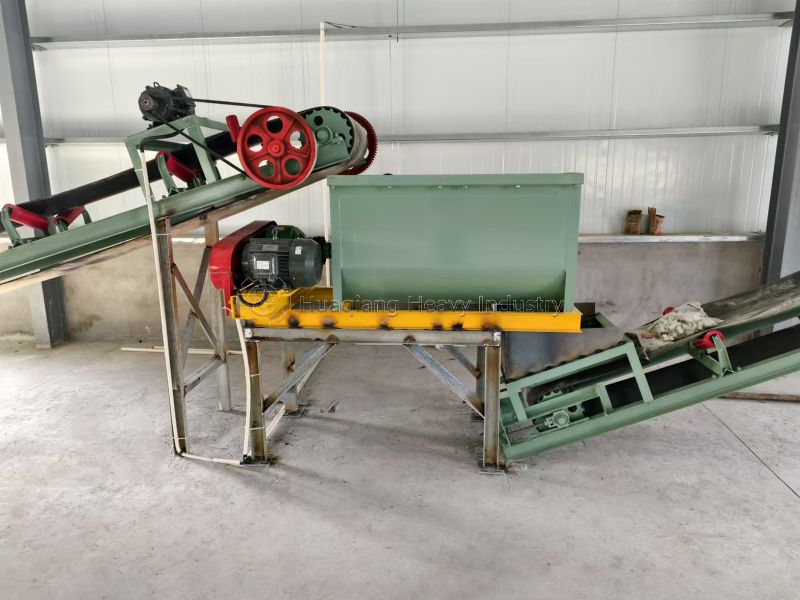
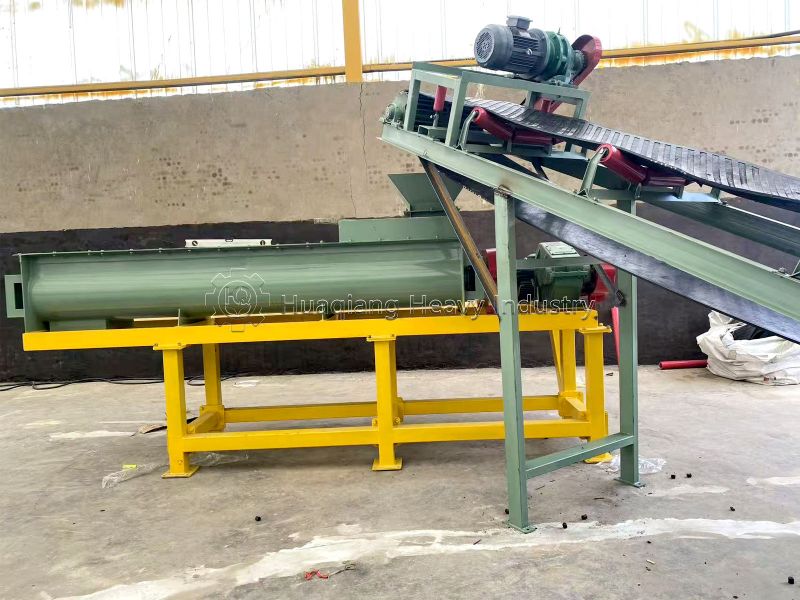
Conveying and lifting equipment, primarily consisting of bucket elevators and belt conveyors, facilitates the transport of materials between different stages of the process. Bucket elevators feed raw materials into the batching silos, while belt conveyors transport the weighed materials to the BB fertilizer mixer. This ensures smooth material handling throughout the process, minimizing the breakage of fertilizer granules, preventing material segregation, and supporting continuous production.
The BB fertilizer mixer is the critical component of the blending stage. Specifically designed for mixing granular fertilizers, it typically employs a horizontal twin-shaft paddle mixer configuration. Inside the machine, materials undergo multi-directional convective tumbling and gentle blending, which ensures that fertilizer granules remain intact. This effectively addresses the challenge of segregation—where particles of varying specific gravities tend to separate—and achieves a level of mixing uniformity that meets the production standards for blended fertilizers. The equipment chamber is designed with minimal "dead zones," resulting in very little material residue; this prevents cross-contamination when switching between different fertilizer formulations. Once mixing is complete, the product is rapidly discharged and conveyed directly to the packaging stage.
The finished-product packaging system consists of an automatic weighing/bagging scale, a bag-sealing machine, and a conveyor belt. After mixing, the fertilizer is automatically weighed and dispensed into bags, which are then sealed and transported for palletizing. This system offers high packaging speeds and precise, stable weighing, accommodating standard fertilizer bag sizes such as 20kg and 40kg.
Overall, a bulk-blended (BB) fertilizer production line requires fewer pieces of equipment, consumes less energy, and entails a lower initial investment compared to compound fertilizer production lines, as it eliminates the need for drying, cooling, and granulation equipment. Enterprises can tailor the production line to their specific scale of operations by adjusting the number of storage hoppers and the specifications of the equipment to match their desired hourly production capacity.